WhatsApp: +86 13530516428 Tel: 0755-23089686     sales@silveroptics.net

Quality Assurance

Home » Quality Assurance

QUALITY CONTROL

Quality Control & Optical Inspection

Plastic optical injection molding

This page outlines inspection topics for injection-molded optical components, including lenses and light guides. The quality plan, test availability, sampling and acceptance criteria must be agreed for the specific material, geometry and application before production.

Explore the quality control process →

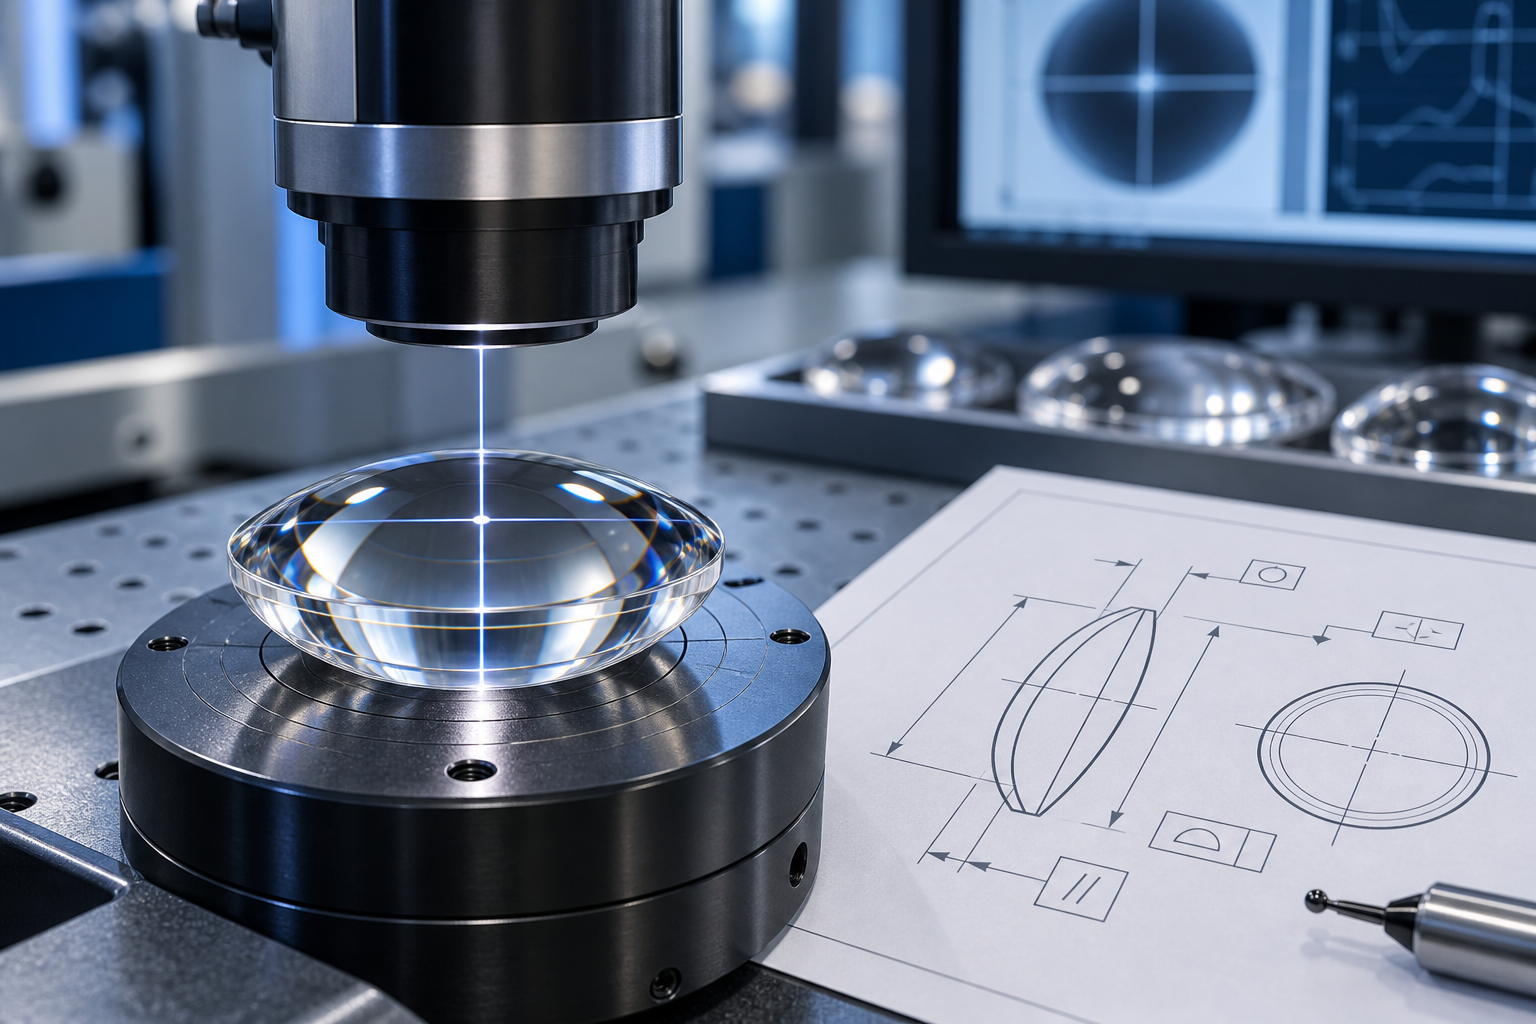
Illustration of optical lens inspection with a measuring head and technical drawings
Optical inspection & measurement
01Optical performance
02Dimensional accuracy
03Surface quality

Quality control across production

Pre-production quality control

  • Raw Material InspectionVerify the conformity of optical plastic materials (PMMA, PC, COP, COC, etc.) with technical specifications, including purity, moisture content, melt flow rate (MFR), and optical transmittance. Reject materials with impurities or inconsistent properties.
  • Mold QualificationInspect mold surface finish, dimensional accuracy of cavities/gates, and cooling system uniformity. Specify the surface roughness parameter, measurement area and acceptance limit for each optical surface during tooling review.

In-production quality control

  • Process Parameter MonitoringReal-time monitor injection molding parameters (mold temperature, melt temperature, injection pressure/speed, holding pressure/time, cooling time) to avoid molded-in stress and optical defects (e.g., birefringence, warpage).
  • In-Process Sampling InspectionConduct periodic sampling of semi-finished products to check preliminary surface quality (no scratches, bubbles, or flow marks) and key dimensions.

Final inspection

  • Final Dimensional InspectionVerify critical dimensions (e.g., lens curvature, thickness, diameter) and geometric tolerance of finished products.
  • Optical Performance TestingEvaluate core optical properties to ensure compliance with specifications.
  • Surface Quality InspectionComprehensive check for surface defects affecting optical performance.

INSPECTION & MEASUREMENT

Inspection and testing equipment

Equipment types are grouped below by inspection purpose. The instrument selection, test availability, measurement conditions and acceptance requirements should be confirmed for each project.

Optical performance & coatings

Spectrophotometer
Spectral transmission and reflection
Transmittance / haze tester
Light transmission and haze
Polarimeter / birefringence meter
Stress-related birefringence
Goniophotometer, reflectometer and abrasion tester
Light distribution, reflectance and coating durability

Surface & dimensional inspection

Laser interferometer
Optical surface form and curvature
Optical profilometer / atomic force microscope
Surface topography and roughness
Coordinate measuring machine / thickness gauge
Critical dimensions and geometry
Optical microscope / optical comparator
Surface appearance, edge profile and visible defects

Materials & process monitoring

Moisture analyzer
Moisture content of molding materials
Melt flow index tester
Material flow behavior
Temperature sensors / pressure transducers
Molding-process temperature and pressure
Process monitoring / visual inspection systems
Process records and defined in-process checks

Reliability & application testing

Temperature / thermal-shock chambers
Temperature exposure and thermal cycling
Humidity chamber / vibration test bench
Humidity and vibration evaluation
Application-specific optical testers
Lighting distribution, endoscope imaging or AR/VR field of view, as applicable
Project-specific test scope
Test availability, conditions and acceptance requirements to be confirmed during review

Inspection methods & acceptance reference

Use the following checklist to define the inspection scope. The equipment listed represents possible measurement methods, not a confirmed inventory or a guarantee of in-house test availability. Acceptance limits, sampling, test conditions and the reporting scope must be agreed for each project.

QC Stage
Inspection Items
Testing Equipment
Inspection Methods & Standards
Pre-Production
Raw material transmittance, moisture content, MFR
UV-Vis spectrophotometer, moisture analyzer, melt flow index tester
  • Transmittance: agree the wavelength range, sample thickness, material grade and acceptance limit
  • Moisture content: follow the specified resin grade requirements and agree the verification method
  • MFR: Comply with material supplier’s specs
Pre-Production
Mold surface roughness, dimensional accuracy
Atomic force microscope (AFM), coordinate measuring machine (CMM)
  • Surface roughness: agree the parameter, measurement area, filtering method and acceptance limit
  • Mold dimensions: verify specified features against the approved drawing and agreed measurement method
In-Production
Injection process parameters
Process monitoring system, temperature sensors, pressure transducers
Define the process parameters to record, approved operating windows, sampling frequency and actions for deviations in the project control plan
In-Production/Final
Surface defects (scratches, bubbles, flow marks)
High-resolution optical microscope, automated visual inspection (AVI) system
  • Visual inspection: agree illumination, viewing conditions, magnification and critical optical zones
  • Inspection coverage and rejection criteria: agree defect types, size limits and sampling before production; confirm automated inspection availability if required
Final
Dimensional accuracy (curvature, thickness, diameter)
Precision CMM, laser interferometer, thickness gauge
  • Dimensional tolerances: follow the approved drawing; agree datums, fixtures and measurement conditions
  • Curvature and surface form: agree the specified quantity, reference surface, aperture and suitable measurement method
Final
Optical performance (transmittance, birefringence, light distribution)
UV-Vis spectrophotometer, polarimeter, goniophotometer
  • Transmittance: agree the spectral range, incidence conditions and acceptance limit for the supplied component
  • Birefringence: agree the measurement quantity, wavelength, optical path and acceptance limit
  • Light distribution: Comply with design specs
Final
Coating quality (if applicable: HC/AR coating)
Abrasion tester, reflectometer
  • Coating durability: agree a suitable test method and acceptance criterion; pencil hardness and abrasion resistance require distinct evaluation methods
  • AR reflectance: agree wavelength range, incidence angle, polarization and whether limits apply per surface or to the component

Quality assurance & traceability

Equipment Calibration

Confirm the calibration or verification status of instruments used for acceptance, the applicable intervals and the records required in the project quality plan.

Personnel Training

Define the training and competency requirements for the inspection methods used on the project.

Data Traceability

Agree the required records and traceability scope, such as material identification, drawing revision, batch references, process records and inspection reports.

Non-Conforming Product Handling

Non-conforming products shall be marked, isolated, and reviewed. Disposition (rework, scrap, re-inspection) shall be approved by the quality department, with preventive measures formulated to avoid recurrence.

Continuous improvement

Review relevant inspection findings, process deviations and customer feedback against the agreed requirements. Define corrective actions, review responsibilities and follow-up records in the project quality plan.

CUSTOMER QUESTIONS

Before samples, production and delivery

What information do you need to review my quality requirements?

Please provide the current drawing revision, 3D model where available, material requirements, critical dimensions and functional optical surfaces. Include the required optical performance, surface appearance criteria, inspection methods, quantities and any coating or assembly requirements. Acceptance limits and measurement conditions should be agreed for the specific component before production.

What should incoming-material inspection cover?

Incoming-material inspection considers conformity with the specified material and the properties relevant to molding and optical performance. These may include material purity, moisture content, melt flow rate and light transmission. Identify the required resin grade, any specified supplier and the operating conditions in your inquiry so the material requirements and verification scope can be reviewed together.

What inspections are relevant during molding and before shipment?

The quality plan should connect process monitoring with in-process and final inspection. Relevant checks include molding temperatures, injection and holding conditions, cooling, critical dimensions, surface appearance and optical performance. Inspection items, sampling frequency, test conditions and acceptance limits need to be defined for the project rather than assumed to be identical for every component.

Which measurement methods are used for different optical requirements?

The appropriate method depends on the feature being evaluated. Interferometry assesses optical surface form; profilometry evaluates surface topography and roughness; dimensional metrology checks geometry; and spectral measurements assess transmission or reflection. Polarimetric methods can evaluate stress-related birefringence. Confirm the required method, measurement conditions and test availability during project review.

How can our incoming inspection be compared with supplier results?

Agree on the measurement method, measurement area, optical and mechanical reference datums, fixtures and relevant test conditions before evaluation. Identify critical optical zones and request a comparable report format. Also distinguish acceptance checks on the supplied component from validation of the completed optical system.

Can I request inspection reports and traceability records?

Please identify the records you need at quotation stage. These may include drawing revision references, material identification, trial sample evaluations, dimensional results and optical test results. Confirm the available documentation, required lot references, report format and any additional testing in the agreed project scope.

What should be reviewed for repeat orders and different production batches?

Identify the approved drawing revision, material and coating requirements, acceptance limits and any changes since the previous order. Where batch comparison is required, specify the lot references and comparable inspection records needed in the project scope.

How should defects or nonconforming parts be handled?

The project quality plan should define how nonconforming parts are identified, segregated and reviewed, along with approval requirements for rework, scrapping or re-inspection. It should also define how findings and corrective actions are recorded. If you identify a concern, contact us with the relevant part or order reference, drawing revision and inspection evidence so the issue can be reviewed against the agreed requirements.

What quality requirements should I specify for coated optics?

Include the substrate material, coating function, operating conditions and required optical performance. Depending on the application, evaluation may address spectral transmission or reflection, surface appearance and coating durability. The applicable test methods, acceptance limits and any environmental testing should be confirmed for the project.

How are packaging and delivery requirements agreed?

Include handling, packaging and delivery requirements in your inquiry, particularly where exposed optical surfaces need protection. These requirements should be reviewed alongside coating, assembly and inspection needs before production release. Send your project information to sales@silveroptics.net or use our Contact Us page. Please arrange confidentiality requirements before sharing sensitive design files.

Share your quality requirements

Send your drawings, optical specifications and inspection requirements for review.

Discuss your project →