- Optical Molds
- OPtical Coating
- Optical Molding
- Optical Tooling
- Tooling Videos
- Prism & Filters
- Custom Optical Parts
- Lighting & Illumination
- Medical & Endoscopy
- Optical Applications
- Automotive Optics
- Imaging & Vision
- Optical Capabilities
- Products & Applications
- Resource
- Custom Glass Optics
- Consumer Electronics
- Industrial Vision
- Aspheric Lenses
- Spherical Lenses
Choosing an Optical Mold: Process, Cavities and Validation
Inquiry- Description
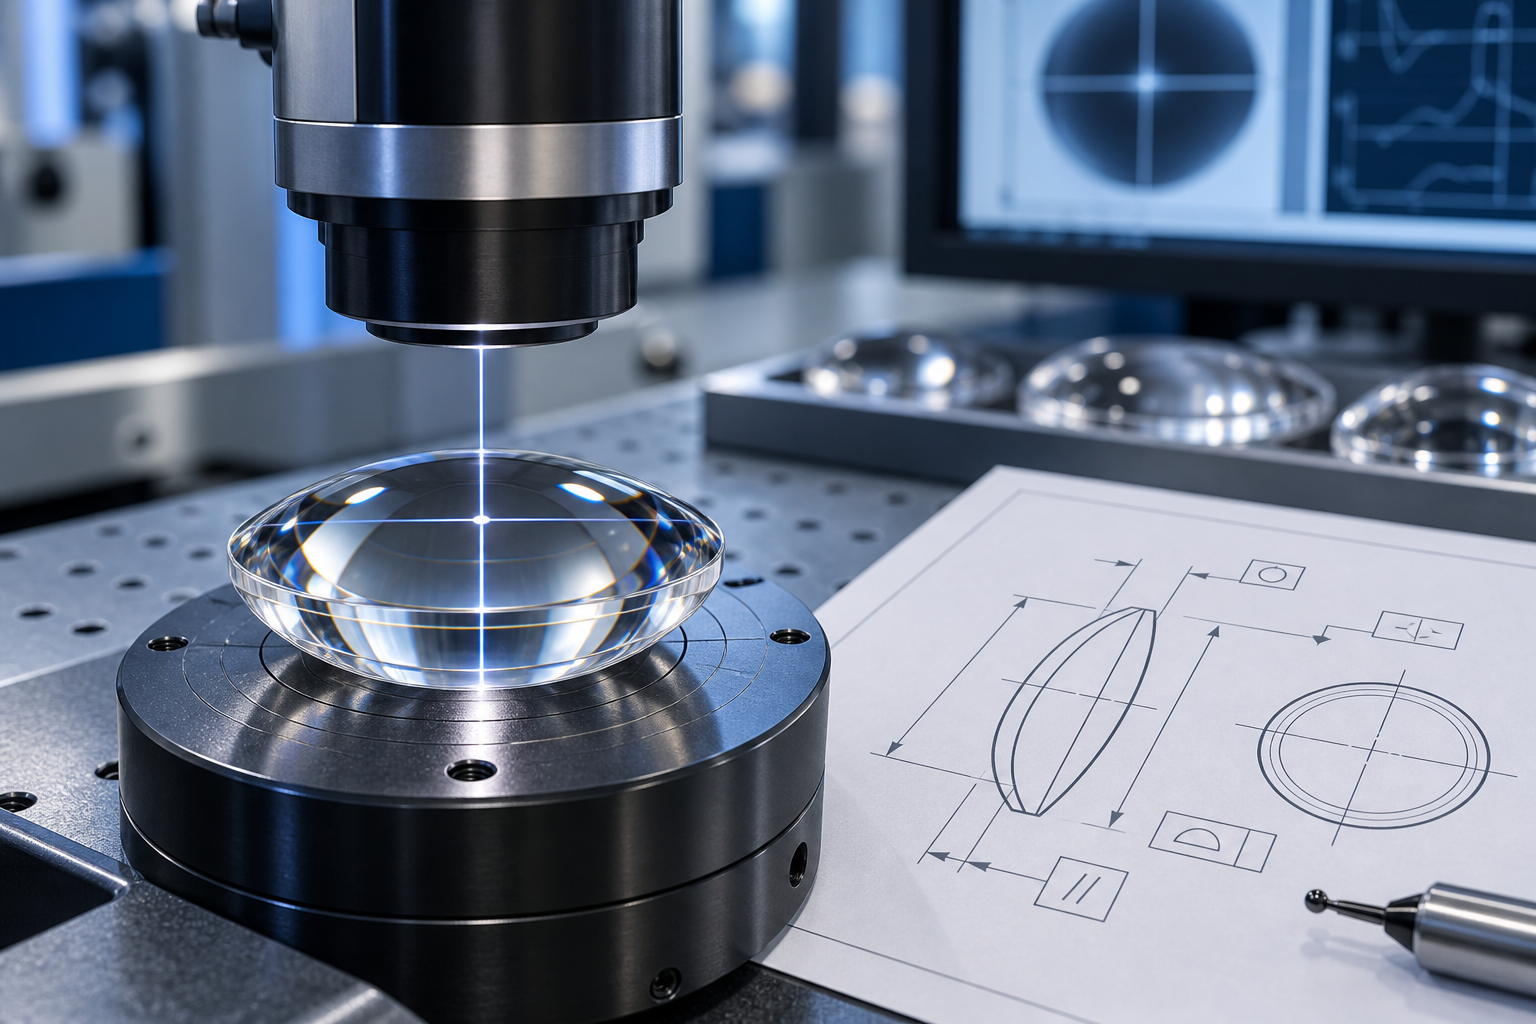
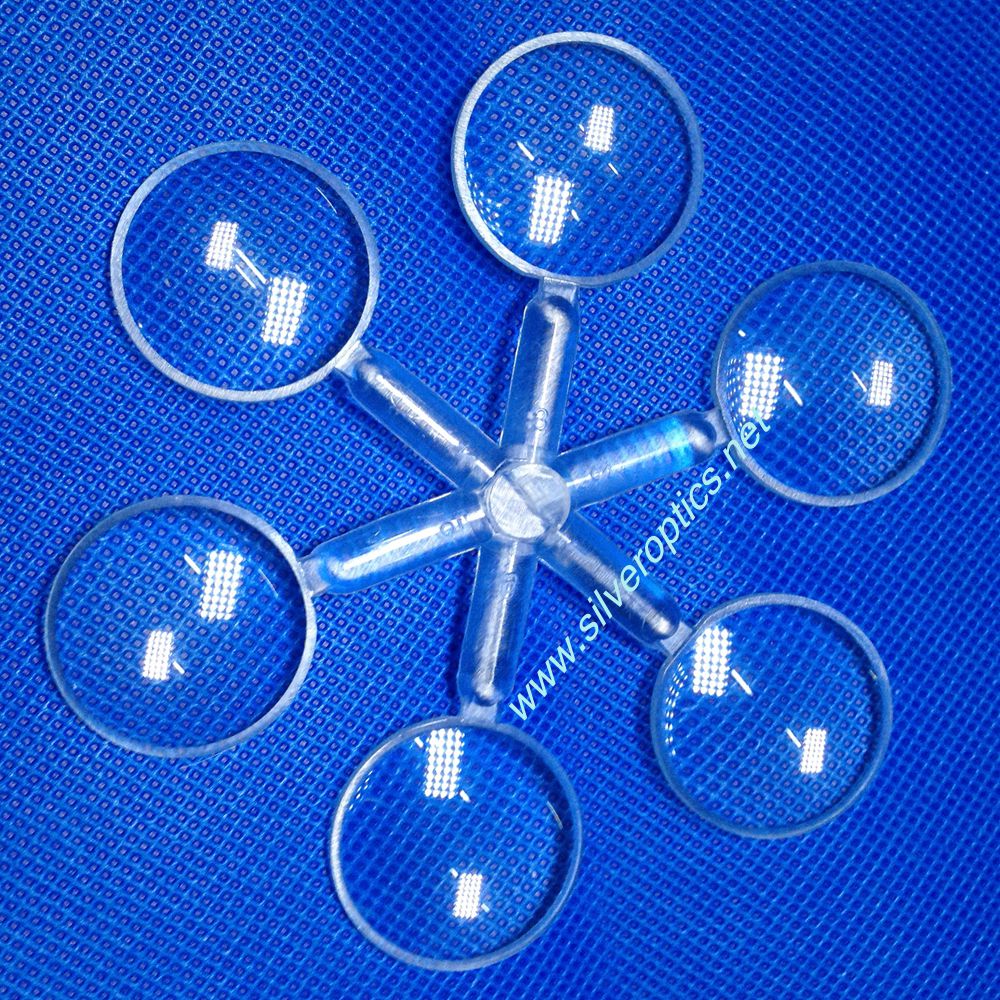
Image: Optical mold-insert illustration.
Choosing an optical mold involves more than selecting a cavity count or a surface-finish label. The tool must reproduce the required geometry with the intended material, while allowing the resulting optical performance to be verified.
Define the surfaces that control performance
An imaging lens, LED optic and light guide may require different geometries and tests. Mark the optical aperture, functional surfaces and assembly datums on the drawing. Identify where gate, ejection and parting-line marks are permitted.
Specify surface form, roughness and local defects separately. A single description such as “mirror finish” does not define all three, and a universal “precision grade” cannot replace the component specification.
Match the process to the geometry
In injection molding, polymer fills the tool cavity before packing and cooling. Thick sections and long flow paths affect the processing challenge, so the optical geometry and proposed molding route should be reviewed together.
Injection-compression introduces controlled cavity movement during the cycle. In suitable designs, it can change the pressure distribution and help reduce residual stress. It also requires coordinated tool and machine behavior, including cavity sealing and the compression sequence. Its benefit should be demonstrated on the required part.
Other forming or replication methods may suit particular materials or surface structures. Select the route from geometry, material and trial evidence rather than assuming one method always gives the best optical result.
Evaluate cavity strategy beyond output
A single-cavity tool can simplify development and identification of a trial issue. A multi-cavity tool increases parts per cycle, but each cavity must be assessed for consistency. Balanced filling and temperature control matter because differences between cavities can produce different part results.
A family tool combines different components. Their filling, packing and cooling needs may differ, so the cycle must be evaluated for the complete set. Cavity count by itself does not establish achievable precision.
Specify the evidence needed for release
Agree how critical insert surfaces and molded parts will be measured. For a multi-cavity tool, retain cavity identity in the trial records and compare the relevant dimensional and optical results across cavities and repeated cycles.
Provide the drawing, resin grade, forecast quantity and acceptance criteria when discussing the tooling scope. Read our optical injection mold overview and optical mold quality guide for the related review requirements.
Consumer Electronics, Blogs, Case Studies
SEND INQUIRY
Related Products
© Silveroptics 2026. All rights reserved
Powered by Silveroptics
Service
