- Products & Applications
- Resource
- Custom Glass Optics
- Optical Molds
- OPtical Coating
- Optical Molding
- Optical Tooling
- Tooling Videos
- Prism & Filters
- Custom Optical Parts
- Lighting & Illumination
- Medical & Endoscopy
- Optical Applications
- Automotive Optics
- Imaging & Vision
- Optical Capabilities
- Consumer Electronics
- Industrial Vision
- Aspheric Lenses
- Spherical Lenses
Optical Plastics and Processes: Match the Material to the Shape
Inquiry- Description
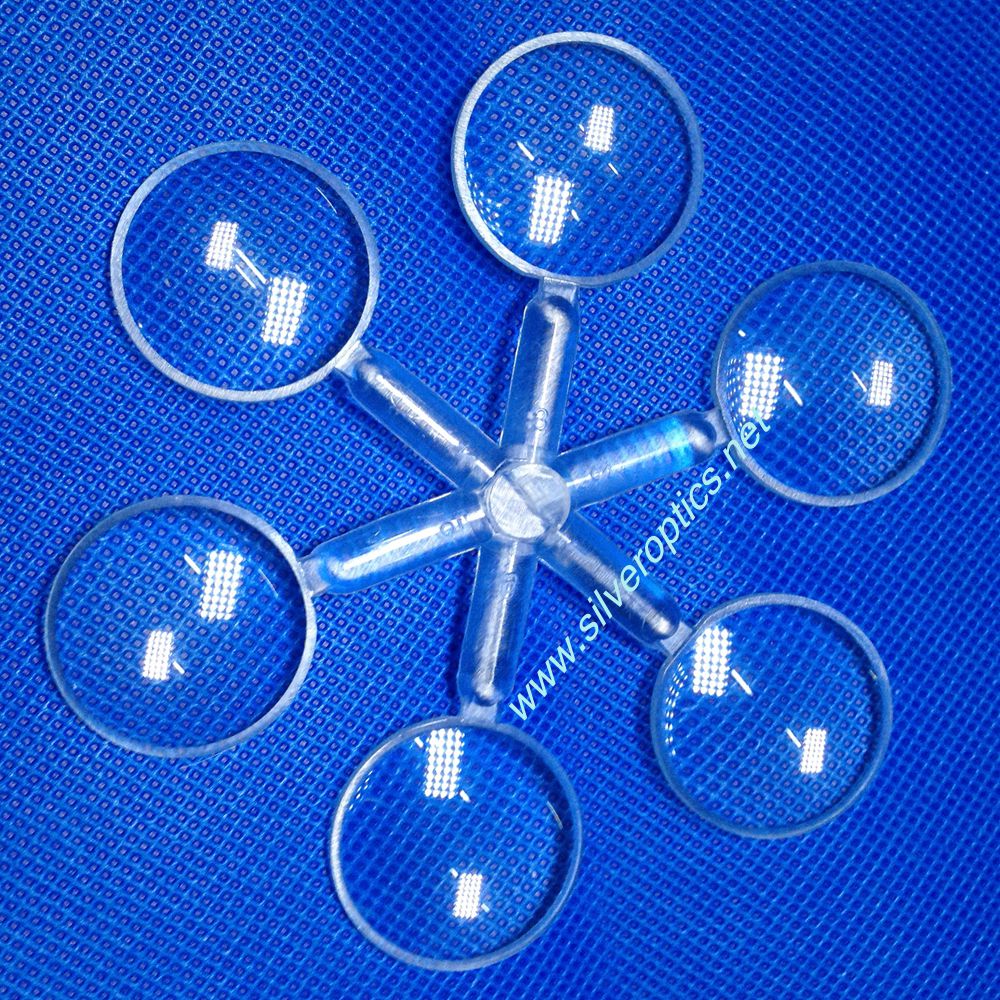
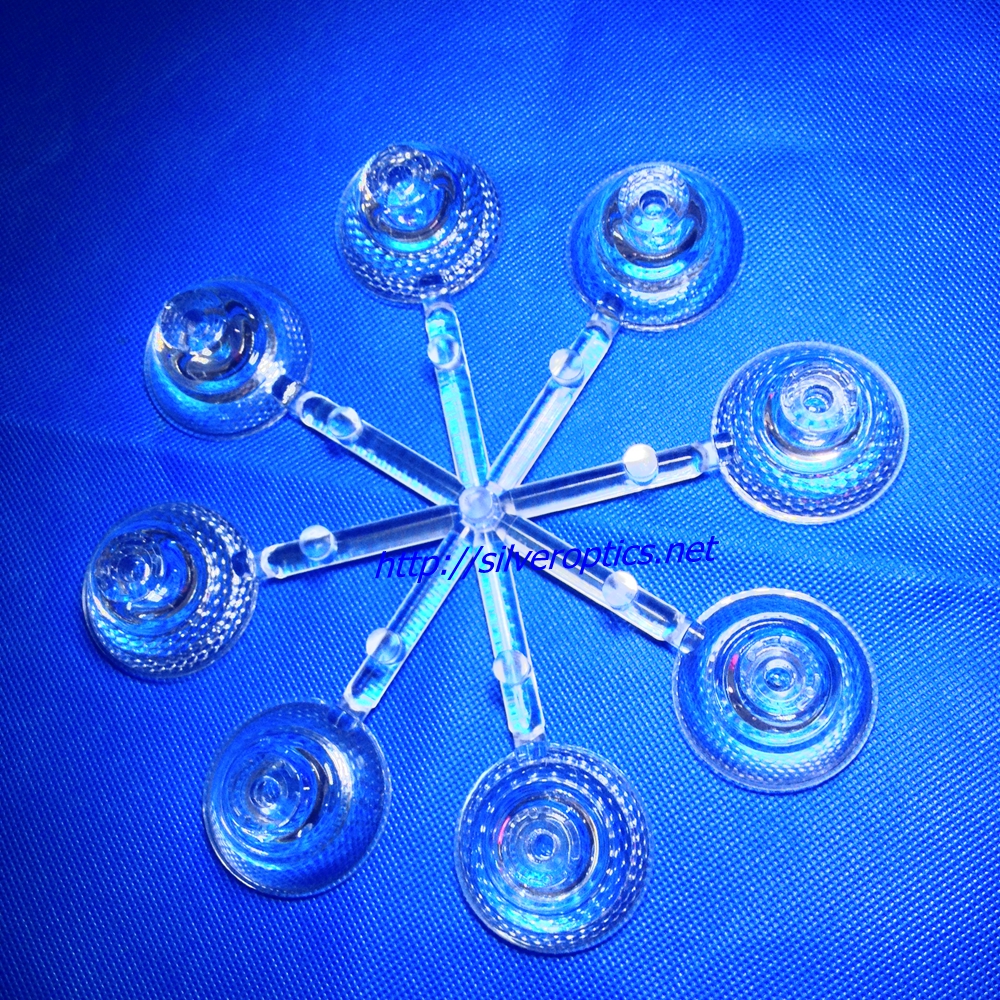
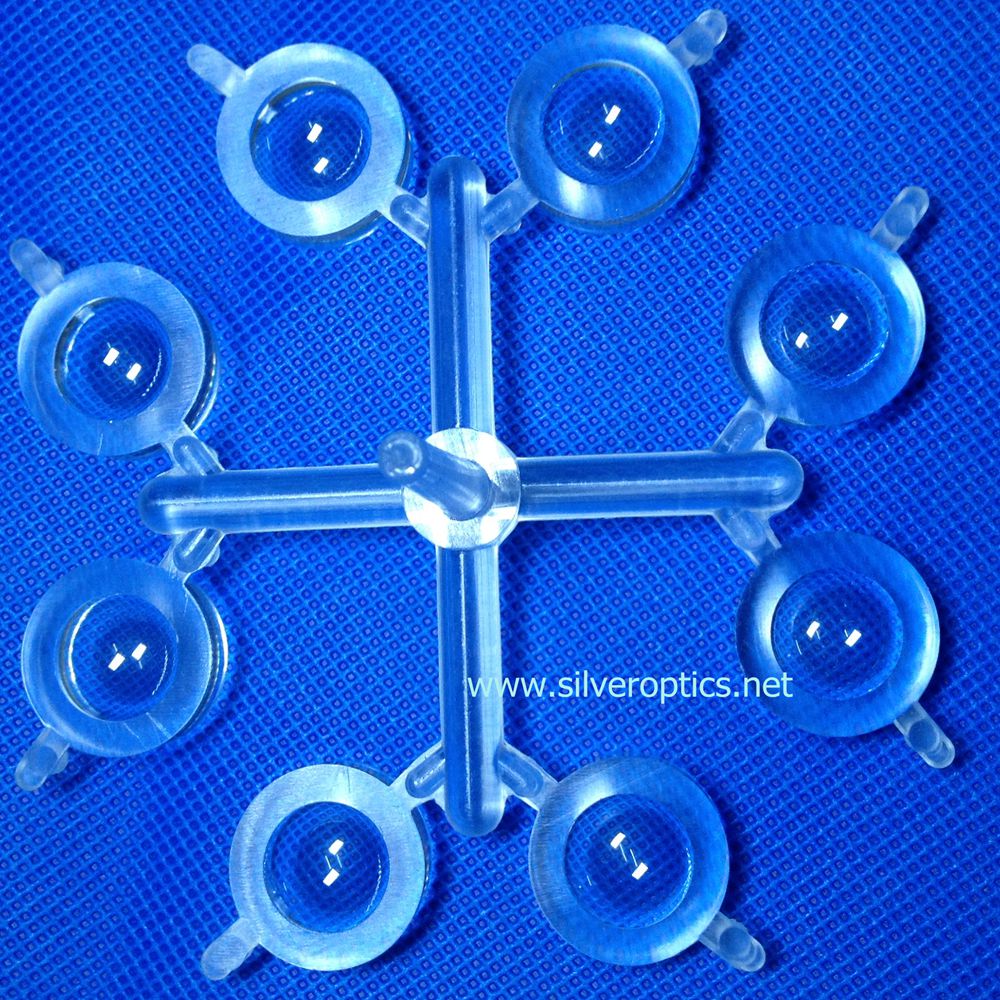
Image: A molded set of optical components illustrates the replication process.
Should the material or manufacturing process be selected first for a plastic optical component? They are connected decisions. A resin with suitable optical data must also fill or form the required geometry and retain that shape after cooling, release and assembly. The most useful starting point is the feature that controls the light.
Choose a material family for the operating conditions
PMMA is used for transparent optical parts and light guides; grade selection affects processing and environmental behavior. Polycarbonate can be useful where impact resistance is important, with optical grades selected for the task.
Optical COP and COC grades offer low moisture absorption and differing combinations of optical and thermal properties. Their birefringence response must be considered with the stress introduced by forming and mounting.
Optical silicones provide another route, particularly for lighting, with forming and curing requirements different from thermoplastics. A material-family name cannot establish coating compatibility or fitness for a particular exposure. The optical plastic properties guide explains which properties need to be connected to the optical requirement.
Match replication to the geometry
Injection molding fills a cavity with molten thermoplastic. It can reproduce optical surfaces and adjacent mechanical features in the same part. Filling, packing, cooling and demolding influence how closely that part follows the intended shape.
Compression molding presses heated material into a tool. Injection-compression combines filling with a compression step. These routes require evaluation of the actual part; a process name alone does not establish lower stress or better accuracy.
Hot embossing transfers structures from a heated tool into a polymer surface. For micro-optical patterns, feature depth, spacing and profile may be more useful inspection targets than the overall part dimensions.
Plan gates, parting lines, release features and optical apertures together during optical mold development. A feature that is convenient mechanically may make filling or release more difficult.
Inspect replication and optical function
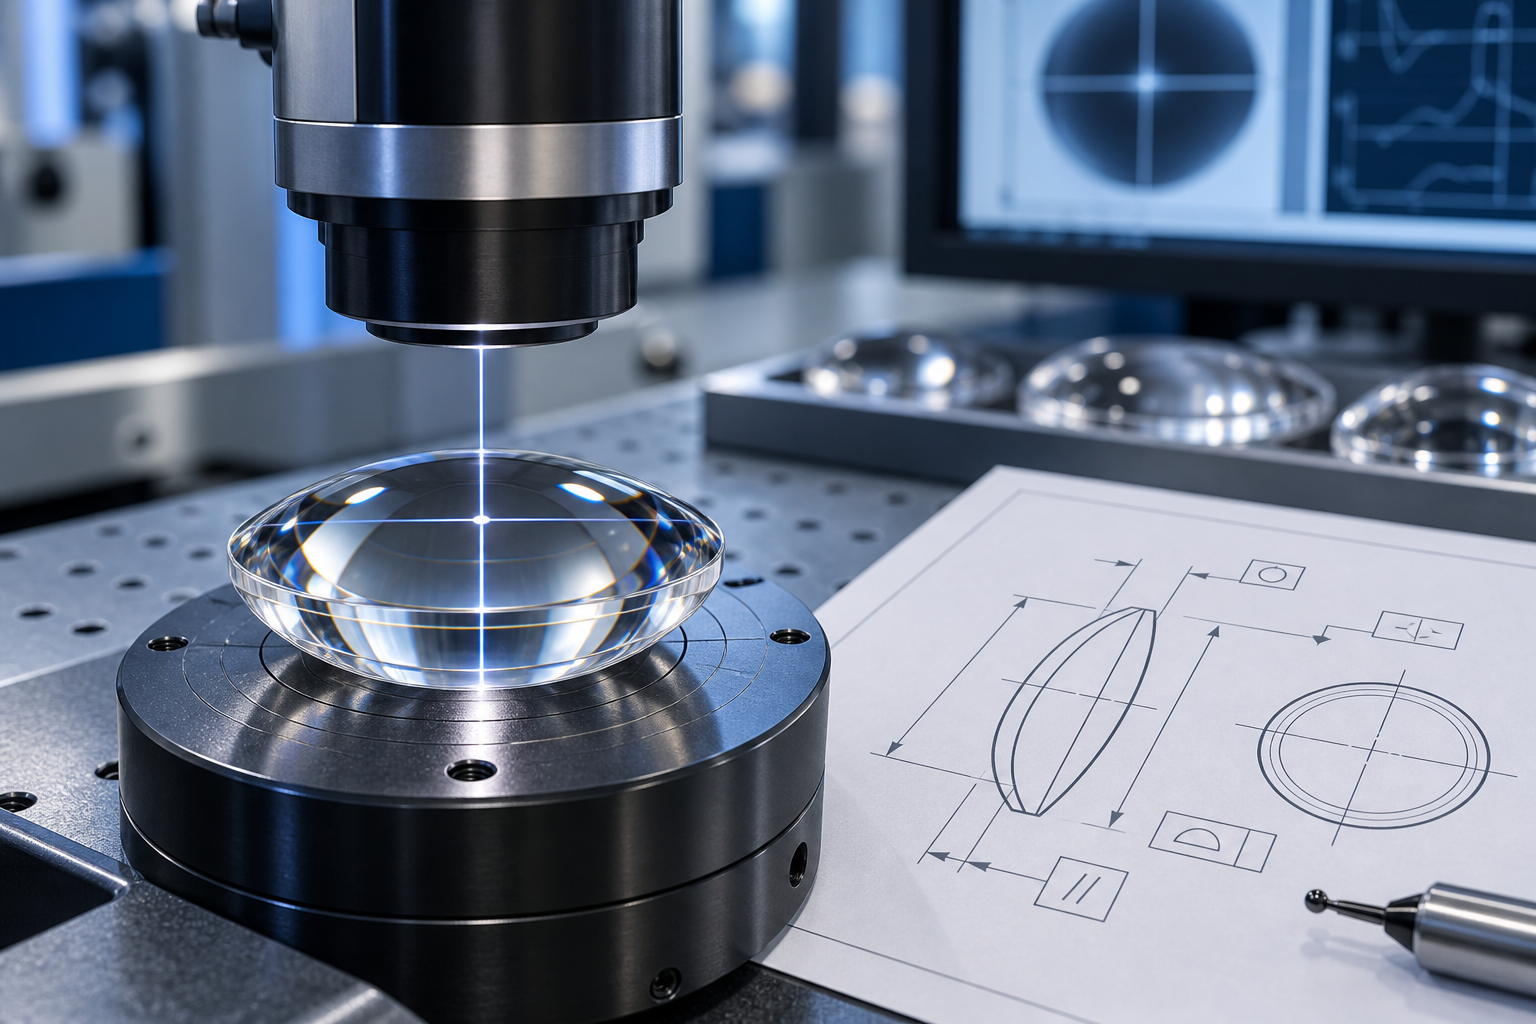
Compare the critical surface or microstructure with its design using suitable profilometry or optical metrology. Measure mechanical locating features separately, and assess birefringence when stress could affect the application.
Then test the function the structure is intended to provide, such as focus or light distribution. Check representative parts after required coatings and mounting steps. This connects the material and process choices to evidence of a usable optical component rather than relying on a visually faithful replica.
Consumer Electronics
SEND INQUIRY
Related Products
© Silveroptics 2026. All rights reserved
Powered by Silveroptics
Service
